Bridgeport Series I Manual Overview
Bridgeport Series I manuals are freely downloadable in PDF, TXT, or online view. They cover installation, operation, maintenance, troubleshooting, and a full parts list. The PDFs include serial-number guidance, safety isolation steps, and feed-selection details for J-series machines. Get PDFs via site today.
What is the Bridgeport Series I?
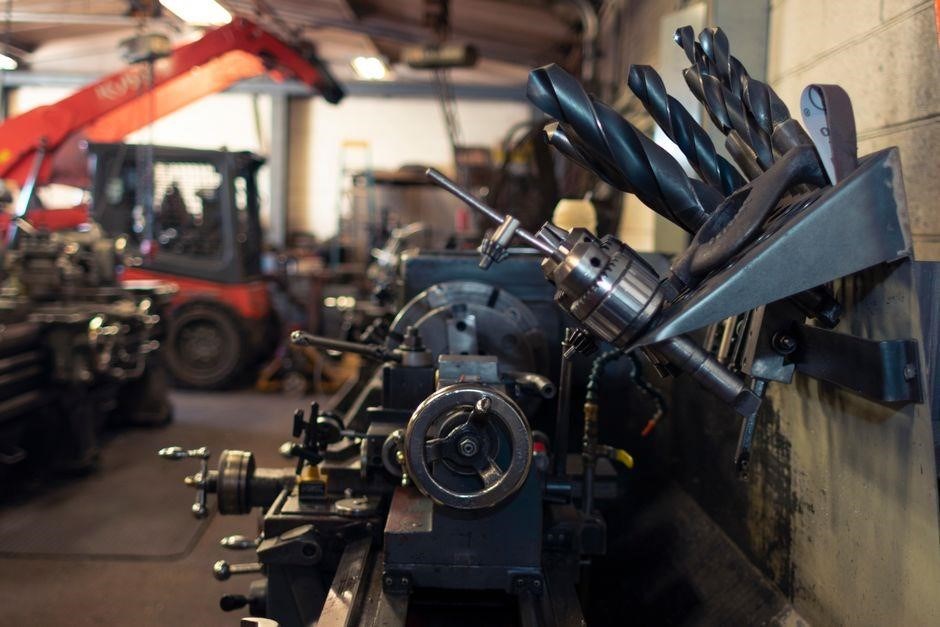
The Bridgeport Series I is a classic precision milling platform that has served workshops worldwide since the 1930s. Its robust cast‑iron frame, adjustable table, and dual‑spindle design provide a versatile work‑horse for shaping metal, wood, and composites. The machine’s modular construction allows for easy upgrades, such as adding a ball‑spindle or a CNC controller, while retaining the original manual controls. With a 12‑inch table travel and a 12‑inch spindle travel, the Series I can accommodate a wide range of workpieces. The spindle speed ranges from 0 rpm to 5,000 rpm, and the feed system offers three selectable rates—1.5, 3, and 6 thousandths per revolution—controlled by a simple crank on the front panel. Safety features include a built‑in interlock that prevents spindle rotation when the guard is open, and a manual clutch that can be disengaged for maintenance. The machine’s design emphasizes durability: the cast‑iron base resists vibration, and the power‑feed system uses high‑quality gears to deliver smooth, repeatable motion. Whether used in a small shop or a large fabrication facility, the Bridgeport Series I remains a reliable and cost‑effective solution for a wide array of machining tasks.
Introduced during the early 20th century, the Series I was originally designed for small‑scale production and rapid prototyping. Its compact footprint (approximately 4 ft × 3 ft) made it suitable for limited shop space, while its sturdy construction allowed it to withstand heavy‑duty operations. Over the decades, the machine has earned a reputation for reliability, with many units still in operation after 80 years of service. The original manual controls—hand‑wheel, throttle, and feed selector—provide intuitive operation for experienced machinists, while the optional electronic controller can be retrofitted for modern CNC applications. The machine’s modularity also means that parts such as the spindle, table, and feed system can be replaced individually, extending the life of the entire platform. For hobbyists, the Series I offers a low‑cost entry into milling, while professional fabricators appreciate its precision and ease of maintenance. Its enduring legacy makes it a staple in both educational institutions and commercial workshops. Collectors value its original tooling and the distinctive brass throttle!!.
PDF Availability and Download Sources
Bridgeport Series I manuals are available as free PDFs, TXT files, or online readers. Users can download the full Series I Manual from the official Bridgeport support portal or trusted third‑party sites that host legacy machine documentation. The PDF includes all sections—installation, operation, maintenance, and parts list—while the TXT version is ideal for quick reference or printing. For those who prefer instant access, the manual can be viewed directly in the browser via the “Read Online” link. Each download is labeled with the machine’s serial number prefix (e.g., J‑series) to ensure the correct version. Links are typically provided in a simple Download table:
- PDF (1;2 MB)
- TXT (200 KB)
- Read Online
All files are protected by standard web‑security protocols and can be accessed without registration. Users should verify the file integrity by comparing the SHA‑256 checksum listed on the download page. The manual is freely distributed under a non‑commercial license, allowing engineers, technicians, and hobbyists to keep a local copy for reference or archival purposes. Users may also convert the PDF to a searchable format using OCR tools or embed the text in a database for lookup. The manual’s coverage ensures legacy Bridgeport Series I machines remain operable and maintainable after models enter production.
Installation Guide
Download the Bridgeport Series I manual PDF, then follow step‑by‑step assembly instructions. Isolate the machine electrically, level the frame, secure the base, spindle, and headstock. Torque bolts to spec and run a test cut to confirm alignment. Ensure bolts are tightened to manufacturer torque specs before operating!!
Site Preparation and Safety Precautions
Before installing a Bridgeport Series I milling machine, the work area must be cleared of debris, tools, and any obstructions that could impede movement or pose a tripping hazard. The floor should be level and free of oil or coolant spills to prevent slips. Adequate lighting is essential; use portable LED fixtures if the existing illumination is insufficient.
Electrical safety is paramount. Verify that the machine’s power supply matches the local voltage and frequency specifications. The main circuit breaker should be isolated, and a lock‑out/tag‑out device applied to the power source before any wiring or maintenance work begins. Grounding straps must be attached to the machine frame and the earth ground to eliminate static discharge risks.
Personal protective equipment (PPE) is mandatory. Operators and technicians should wear safety glasses, hearing protection, and steel‑toed boots. When handling heavy components, use proper lifting techniques or mechanical aids to avoid back injury. A fire extinguisher rated for electrical and metal fires should be positioned within arm’s reach.
For ventilation, ensure that the machine’s coolant system is properly vented and that any fumes are directed away from the work zone. Install a spill containment mat beneath the coolant reservoir and a fire extinguisher rated for electrical and metal fires. Finally, document all safety checks in a logbook and obtain sign‑off from the site supervisor before powering the machine. Review annually. Staff.!!
Step-by-Step Assembly Instructions
- Verify all structural components—base, column, headstock—are present, clean, and undamaged. Place base on level surface, align four corner holes, and secure with M12 bolts. Tighten each to 80 Nm, alternating for even clamping.
- Attach column to base using 8‑bolt set (M10). Use a dial indicator to confirm vertical alignment before tightening. Lock bolts to 70 Nm.
- Install headstock onto column. Align spindle shaft with column shaft, ensuring no play. Insert 1/4‑20 shoulder bolt; torque to 25 Nm. Verify headstock rotates freely.
- Thread main drive shaft through headstock bearing. Apply thin grease to bearing surface, insert shaft, and tighten drive bolt to 60 Nm.
- Mount tailstock onto column. Adjust tailstock height to maximum travel, lock adjustment screw, and test smooth travel by moving tailstock manually. Check for any binding;
- Attach milling head to headstock. Tighten mounting bolts (M8) in star pattern to 30 Nm. Confirm head rotates without wobble.
- Install power feed system. Connect drive cable to motor housing, route it away from moving parts, and secure with cable ties. Verify cable is tensioned but not overstretched.
- Fit spindle motor. Align motor shaft with spindle shaft, insert motor, and tighten mounting bolts (M10) to 35 Nm. Check proper alignment by rotating motor manually.
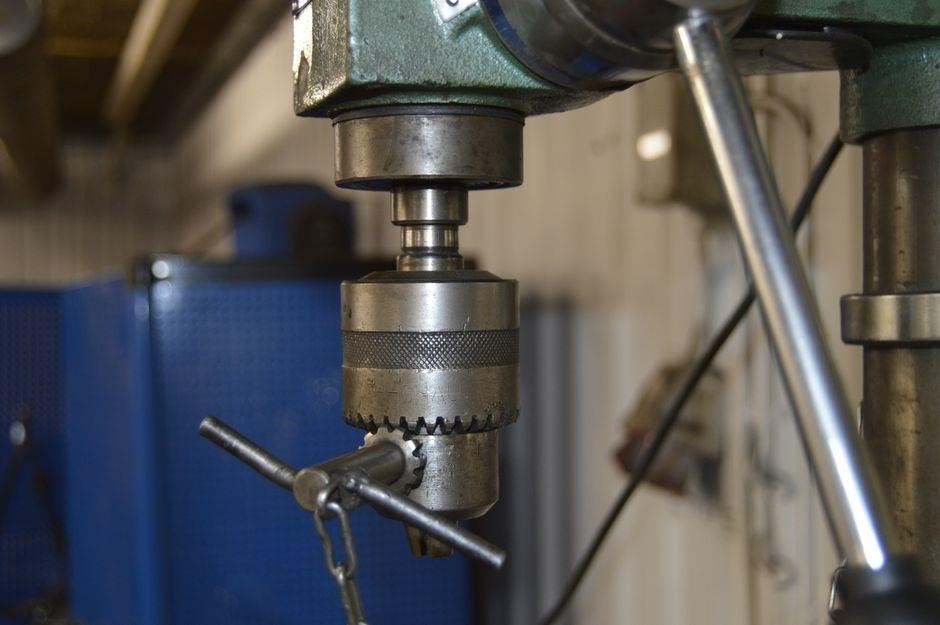
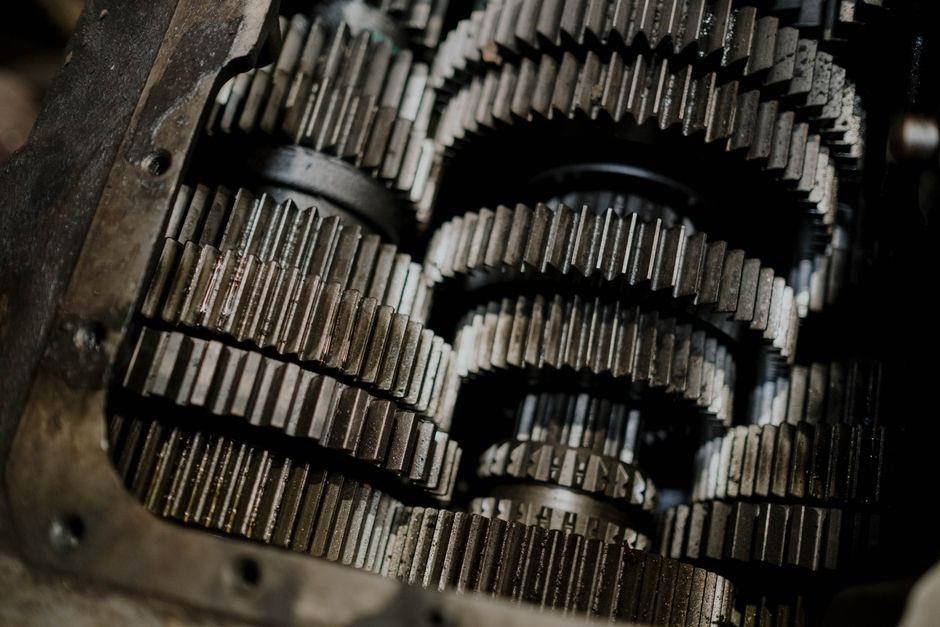
After assembly, perform a dry run by rotating the spindle manually to ensure free movement, then engage the motor to test the power feed. Adjust the feed selector to 1.5 mm/rev, 3 mm/rev, and 6 mm/rev to confirm operation. Document steps in the logbook and proceed to the operation manual. All bolts are torqued to spec. Check alignment with dial indicator!OK
Operation Manual
Bridgeport Series I operation manuals detail feed selection, spindle speed, and tool change procedures. The PDF covers safety isolation, control panel navigation, and the three feed settings (1.5, 3, 6 thou/rev). Users can download the file for quick reference. The manual also explains spindle speed limits now.
Operating Controls and Settings
Operating controls on a Bridgeport Series I are arranged for intuitive use. The main control panel sits at the front of the machine and is divided into three sections: the handwheel area, the feed selector, and the speed control. The handwheel, located on the left side, allows the operator to move the spindle and table in the X, Y, and Z directions. Each wheel has a numbered index that corresponds to the mill’s travel limits; the index is calibrated in thousandths of an inch. The feed selector is a three‑position lever that sets the feed rate to 1.5, 3, or 6 thousandths per revolution. To change feeds, pull the knob out, rotate it to the desired position, and release it; the lever locks into place automatically. The speed control is a dial that ranges from 0 to 10 rpm. The dial’s markings are in increments of 0.5 rpm, and the machine’s internal governor ensures that the spindle speed does not exceed the selected value. A separate lever on the right side of the panel controls the coolant system; pushing the lever forward activates the coolant pump, while pulling it back shuts the system off. The control panel also includes a small LED display that shows the current spindle speed, feed rate, and coolant status. All controls are designed to be operated with one hand, allowing the operator to keep the other hand on the workpiece. Proper use of these controls ensures smooth operation and maximizes tool life. Operators should consult the manual for calibration details. All settings are adjustable to meet specific machining needs.
Additional controls enhance machining precision and safety. Beneath the feed selector sits a depth‑of‑cut lever that adjusts the cut depth in 0.001‑inch increments, with a spring‑loaded detent holding the selected value. A quick‑release clutch lever disengages the spindle from the motor for rapid tool changes; pulling the lever stops the spindle immediately, and releasing it re‑engages the motor. An emergency stop button, labeled “E‑STOP,” is positioned near the top of the panel; pressing it trips an internal relay that cuts power to the spindle and motor, allowing instant shutdown. A small indicator light illuminates when the machine is operating, providing a visual cue that the spindle is running. Familiarizing operators with these controls and settings leads to accurate, efficient, and safe machining performance on the Bridgeport Series I.
Feed Selection and Gearing Information . .
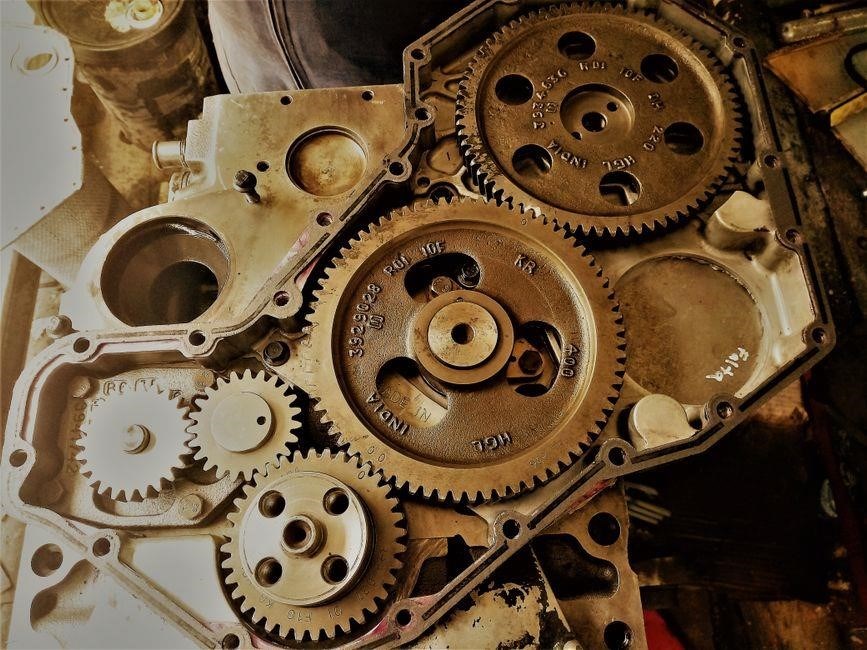
The Bridgeport Series I manual details the three standard feed rates selectable via the crank on the left side of the machine. Each position corresponds to a specific gear ratio that drives the spindle and table feeds. The first position (1.5 thousandths per revolution) uses a 1:1 gear set, the second (3 thousandths) engages a 2:1 ratio, and the third (6 thousandths) utilizes a 4:1 gear train. The crank’s 1/4‑20 shoulder bolt secures the clutch arm, which houses two roller cams. When the crank is pulled out and rotated, the cams engage the appropriate gear set inside the gear box, ensuring smooth transition between feeds.
To change feeds, first isolate the machine and stop the spindle. Loosen the 1/4‑20 shoulder bolt, remove the clutch arm, and inspect the roller cams for wear. Replace worn cams with OEM parts. Reinstall the arm, tighten the bolt, and test the crank through all positions while observing spindle speed and feed indicator. The manual recommends a calibrated dial gauge to verify the feed per revolution matches the setting.
Gearing information is listed in the parts list section of the PDF. The gear box contains a 12‑tooth pinion, a 24‑tooth gear, and a 48‑tooth gear, matching the 1:1, 2:1, and 4:1 ratios. The manual advises periodic lubrication of the gear teeth with light oil to prevent wear. If the feed feels sluggish, check the gear mesh for binding, clean the gear teeth, and re‑lubricate. Proper gear maintenance ensures accurate feed selection and prolongs machine life. Refer to serial number section for gear specs!
Maintenance & Troubleshooting
Maintenance & troubleshooting sections in the Bridgeport Series I PDF guide list routine checks, common faults, and fixes. It covers clutch arm spring removal, gear alignment, feed‑crank operation, and electrical isolation steps for safe repair. Check bearings, lubricate, and verify spindle speed calibration.! 26.
Routine Maintenance Procedures
Routine maintenance keeps a Bridgeport Series I milling machine running smoothly and extends its service life. Follow the schedule below, using the PDF manual as a reference for detailed torque values and part numbers.
- Daily Checks: Inspect the machine for visible damage, ensure all guard panels are closed, and verify that the spindle speed selector is in the neutral position. Clean the worktable and remove any chips or debris.
- Weekly Lubrication: Apply the recommended grease to the spindle bearings, lead screw, and cross‑slide bearings. Use the supplied grease gun and follow the torque specifications found in the PDF.
- Monthly Inspection: Check the condition of the clutch arm and spring. Verify that the 1/4‑20 shoulder bolt remains tight. Inspect the roller cams for wear and replace if necessary.
- Quarterly Service: Replace the spindle oil filter, inspect the drive belts for tension and wear, and clean the cooling system. Verify that the feed gears are properly aligned.
- Annual Overhaul: Perform a full disassembly of the spindle assembly, clean all components, and re‑apply fresh grease. Inspect the main shaft for straightness and replace any worn parts. Update the machine’s serial number plate if a major component is replaced.
Record each maintenance activity in the logbook supplied with the manual. This documentation not only helps in troubleshooting but also satisfies warranty requirements.
Log maintenance tasks, noting dates, parts replaced, observations. This record assists in repairs and extends machine’s operational life. Keep
Common Issues and Fixes
Common problems with the Bridgeport Series I often stem from wear, improper lubrication, or mis‑alignment. Below are typical symptoms and straightforward remedies that can be found in the PDF manual. First, a sluggish spindle may indicate a worn clutch or insufficient oil in the hydraulic pump; the manual recommends draining the old oil, replacing the filter, and re‑injecting fresh fluid. Second, a noisy or vibrating table usually points to loose bolts or worn table bearings; tightening all fasteners to the specified torque and replacing any damaged bearings resolves the issue. Third, uneven cutting depth can result from a bent or mis‑aligned headstock; the guide shows how to use the built‑in dial indicator to check alignment and how to shim the headstock to correct it. Fourth, a loss of feed accuracy is frequently caused by a worn feed screw or an improperly set micrometer; the PDF details how to disassemble the screw, clean the threads, and re‑tune the micrometer. Finally, a jammed or stuck gear in the feed mechanism often occurs when the gear oil is contaminated; the manual advises removing the gear, cleaning the housing, and refilling with fresh oil. Following these steps, as outlined in the downloadable manual, typically restores reliable operation.
Parts List & Specifications
Key components: spindle, headstock, tailstock, table, feed drive, clutch, gears, cams, and safety interlocks. Serial numbers start with J, model variants differ by feed options (1.5, 3, 6 mm/min). Full list in PDF includes part numbers, dimensions, and torque specs. PDF
Major Component Identification
The Bridgeport Series I manual PDF offers a concise yet exhaustive catalog of each primary part, enabling quick reference for troubleshooting or part replacement. The diagrammatic sections of the PDF use consistent labels that correspond directly to the physical components on the machine. Below is a curated list of the most critical elements, each paired with its official designation as found in the PDF’s parts list.
- Base – The steel frame that supports the entire machine; labeled “B” in the schematics.
- Table – The horizontal surface that moves in X‑ and Y‑directions; marked “T” with cross‑hair alignment.
- Spindle – The rotating head that holds the cutting tool; identified as “S” and accompanied by the speed selector diagram.
- Headstock – The assembly housing the spindle, depth‑stop, and feed‑crank; labeled “HS” and illustrated with the depth‑stop lever.
- Tailstock – The movable counter‑bore aligning with the headstock; marked “TS” and shown with the collet holder reference.
- Feed‑crank – The lever that advances the table; identified as “FC” and depicted with the three‑feed selection positions.
- Depth‑stop – The adjustable stop limiting spindle travel; labeled “DS” and shown with the screw‑adjustment notation.
- Power‑feed lever – The lever engaging the power‑feed system; marked “PF” and illustrated with the gear‑shift diagram.
- Clutch arm – The component disengaging the power feed; identified as “CA” and shown with the spring‑loaded cam.
- Spindle‑gearbox – The gear train driving the spindle; labeled “SG” and accompanied by gear ratios.
Each entry in the PDF’s parts list is cross‑referenced with component numbers used in the assembly instructions, ensuring that users can match textual descriptions to physical parts without confusion. The manual also includes serial‑number tags for every major component, facilitating precise identification during maintenance or repair.
For complete details, consult the PDF’s exploded diagrams and the accompanying parts list, which provide exact measurements and torque specifications for every major component.
Serial Number and Model Variants
Bridgeport Series I milling machines employ a serial‑number scheme that starts with the letter “J” and is followed by a six‑digit numeric code. The first two digits represent the year of manufacture, the next two the month, and the last two the unit’s sequence number for that month. For instance, J210312 denotes a machine built in March 2021, 12th unit of the month. Each machine’s model is identified by a suffix added to the base series number. The original Series I (Model A) featured a 12‑inch table and a 4‑inch spindle. The Series I‑B added a 16‑inch table and a 6‑inch spindle, while the Series I‑C incorporated a 20‑inch table and an 8‑inch spindle. Subsequent revisions—Series I‑D and I‑E—introduced electronic feed‑rate controls and a hydraulic power‑shift clutch. All variants share the same core mechanical architecture, enabling parts interchangeability across models. The PDF manuals provide detailed diagrams of the serial‑number layout, model‑specific features, and recommended maintenance schedules. When ordering replacement parts, reference the full serial number and model suffix to ensure compatibility. For machines with non‑standard serial numbers, consult the “Serial‑Number Lookup” tool on the official website. Common model variations include the Series I‑F, which offers a 24‑inch table and a 10‑inch spindle, and the Series I‑G, featuring a 30‑inch table and a 12‑inch spindle. By accurately identifying the serial number and model designation, technicians can determine the machine’s capabilities, verify part compatibility, and follow the correct operating and maintenance procedures outlined in the downloadable PDF manual.